Industrial automation systems rely on electronics for control, sensing, communication, power management, motion control, signal processing, and machine interfaces.
Depending on the application, PCB assemblies may be used in:
- PLC-related electronics
- Industrial controllers
- Motor drives
- I/O modules
- Sensor interfaces
- Industrial communication equipment
- Robotics
- Machine control systems
- Power control equipment
- Human-machine interface systems
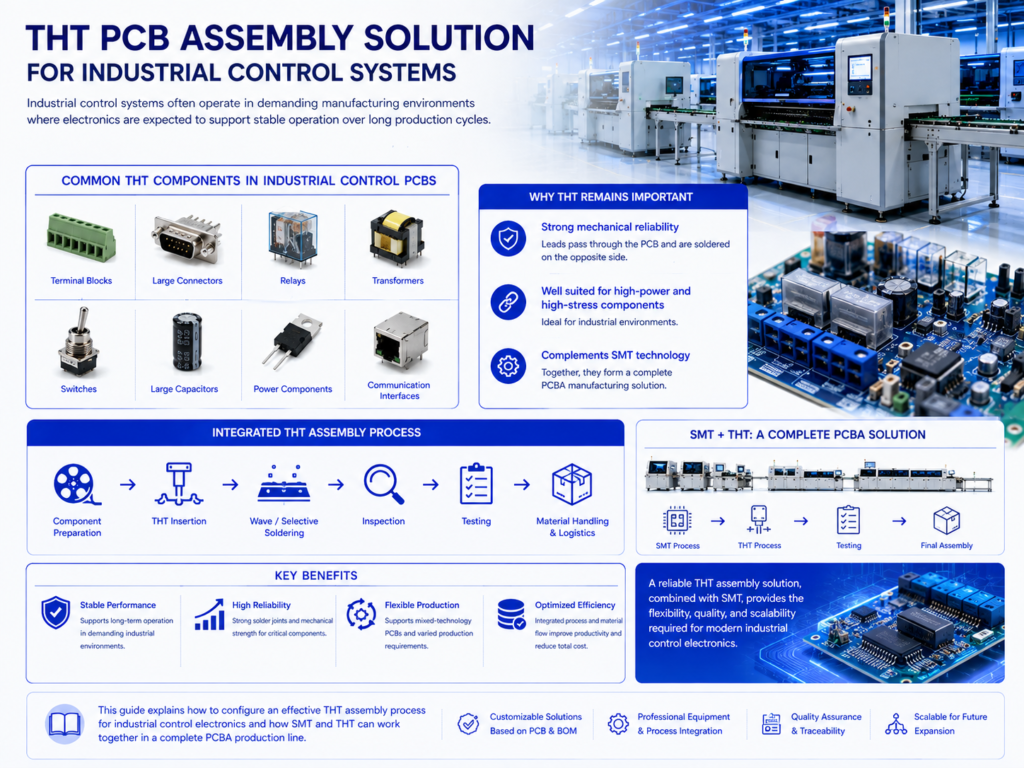
These PCBAs can combine dense SMT control electronics with larger through-hole connectors, relays, transformers, terminal blocks, capacitors, and other electromechanical or power components.
As a result, an effective PCB assembly solution for industrial automation often requires more than a standard SMT line.
A typical mixed-technology manufacturing process may be:
Solder Paste Printing → SPI → SMT Placement → Reflow → AOI → THT Component Preparation → THT Insertion → Wave/Selective Soldering → Inspection → Programming/Testing
Depending on the product, additional processes may include cleaning, conformal coating, traceability, and final functional testing.
The correct solution should be designed around the actual PCB, BOM, product mix, production capacity, quality requirements, and factory layout.
Why Industrial Automation PCB Assembly Can Be Challenging
Industrial automation electronics often combine several manufacturing requirements on the same PCBA.
A board may contain:
- Small SMT passive components
- ICs
- QFPs
- BGAs or QFNs
- Communication components
- Power devices
- Relays
- Transformers
- Connectors
- Terminal blocks
- Large capacitors
- Other THT components
This creates challenges in:
- Component placement
- Thermal processing
- THT insertion
- Soldering
- Inspection
- Testing
- Product changeover
There is therefore no universal production-line configuration suitable for every industrial automation PCB.
Start with the PCB and BOM
Before selecting equipment, analyze the actual product.
Important data includes:
- PCB dimensions
- PCB thickness
- Panel dimensions
- PCB weight
- BOM
- Component packages
- Number of SMT placements
- Smallest SMT component
- Largest component
- Maximum component height
- THT component list
- Component packaging
- Target production volume
This information determines which processes should be automated and which equipment configuration is practical.
Typical Industrial Automation PCBA Production Flow
For a mixed SMT and THT product, a complete process may be:
PCB Loader → Automatic Solder Paste Printer → SPI → Pick and Place Machine(s) → Reflow Oven → AOI → THT Preparation → THT Insertion → Pre-Solder Inspection → Wave or Selective Soldering → Cooling → Inspection → Testing
Optional processes can include:
Cleaning → Conformal Coating → Curing → Final Inspection
Not every industrial automation PCB requires every process.
Step 1: Solder Paste Printing
Solder paste printing establishes the solder deposit for SMT components.
Important process factors include:
- Stencil design
- Solder paste
- PCB support
- Alignment
- Squeegee parameters
- Separation
- Stencil cleaning
For automated production, an inline solder paste printer can provide programmable and repeatable operation.
The printer should be selected according to PCB dimensions, required process capability, production volume, and product mix.
Step 2: SPI
SPI can inspect solder paste characteristics before placement.
Depending on the equipment, measurements may include:
- Height
- Volume
- Area
- Position
SPI can help identify printing variation before the PCB receives components and enters reflow.
This can be particularly useful for industrial PCBAs containing dense SMT layouts or fine-pitch components.
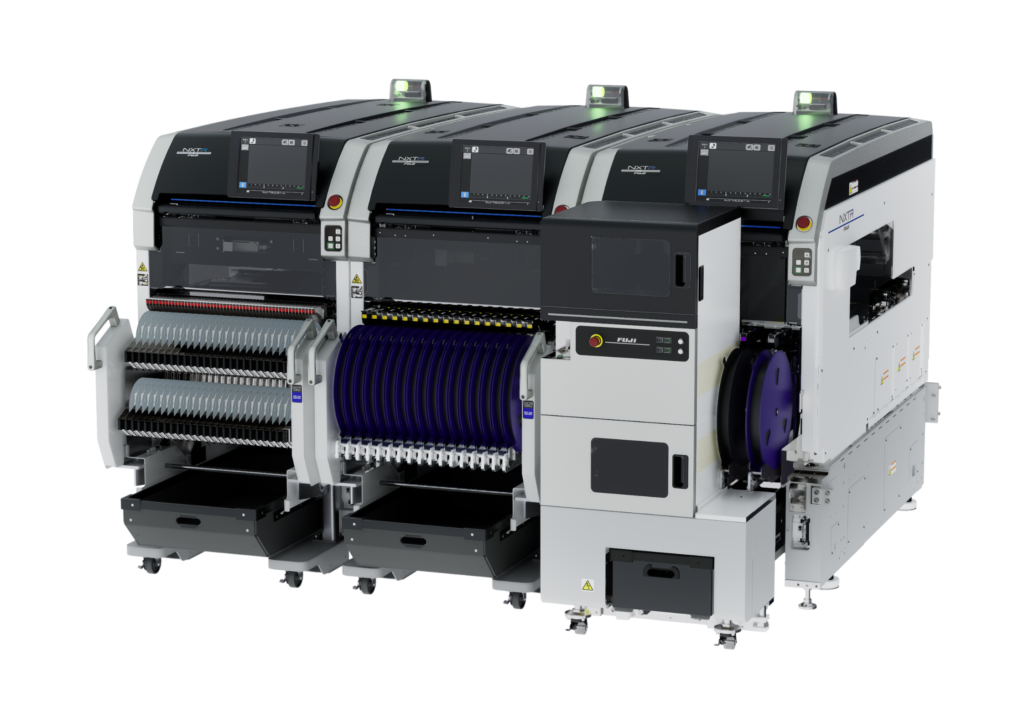
Step 3: SMT Placement
Industrial automation PCBAs can contain a broad component range.
The pick and place machine should be evaluated for:
- Smallest component
- Largest component
- Placement accuracy
- Component height
- Feeder capacity
- Tray components
- PCB dimensions
- Placement quantity
- Product changeover
Nominal CPH alone should not determine machine selection.
Placement Capacity Example
Suppose an industrial control PCB contains: 400 SMT placements
and the required output is: 100 boards/hour
The theoretical placement requirement is: 400 × 100 = 40,000 placements/hour
However, actual machine requirements should also account for:
- Component mix
- Feeder arrangement
- Recognition
- Tray components
- PCB transfer
- Machine efficiency
The machine should therefore be selected using the actual BOM rather than the theoretical number alone.
High-Mix Industrial Electronics Production
Industrial automation factories may manufacture many PCB models in relatively small or medium batches.
In this environment, priorities may include:
- Large feeder capacity
- Fast changeover
- Offline feeder preparation
- Recipe management
- Flexible component handling
- Tray support
- Component verification
Maximum catalog placement speed may be less important than effective production time across multiple product changes.
Step 4: Reflow Soldering
After placement, the PCB enters the reflow oven.
The thermal process depends on:
- Solder paste
- PCB construction
- Copper distribution
- Component requirements
- Thermal mass
Industrial control PCBAs may contain large copper areas or heavier components that affect thermal behavior.
There is no universal reflow profile for industrial automation PCBs.
Actual boards should be thermally profiled during process development.
Thermal Mass Matters
A PCB containing:
- Large copper planes
- Power components
- Connectors
- Shields
- Large inductive components
may heat differently from a small low-mass control board.
The oven should provide sufficient process flexibility for the actual product range.
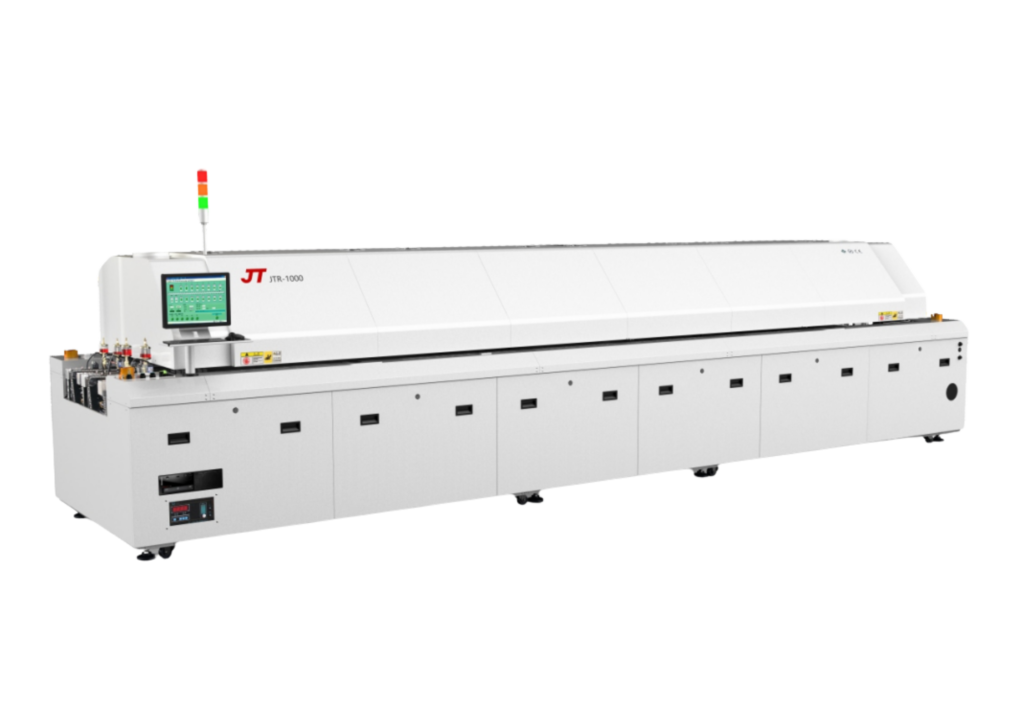
Step 5: AOI
After reflow, AOI can inspect visible assembly characteristics such as:
- Missing components
- Position
- Polarity
- Orientation
- Certain visible solder-joint conditions
- AOI can support process monitoring and defect detection.
However, AOI cannot directly inspect every hidden solder structure.
When Should X-Ray Be Used?
X-ray may be considered for selected hidden solder joints, such as:
- BGA
- Certain QFN applications
- Other packages where optical access is limited
- Not every industrial automation PCB needs X-ray inspection.
The inspection strategy should follow the component structure and product requirements.

Step 6: THT Component Preparation
Many industrial automation PCBAs contain through-hole components.
Typical examples can include:
- Terminal blocks
- Connectors
- Relays
- Transformers
- Large capacitors
- Inductors
- Switches
- Selected power components
Before insertion, some components may require:
- Lead cutting
- Lead forming
- Bending
- Straightening
- Sorting
- Kitting
Component preparation should be considered part of the production line because it can become a hidden bottleneck.
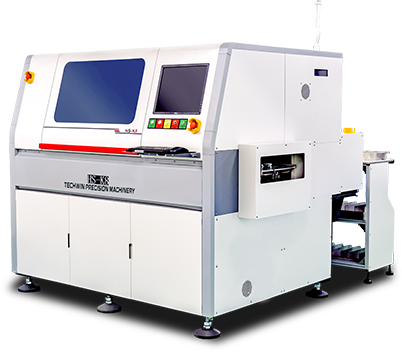
Step 7: THT Insertion
THT components can be inserted:
- Manually
- Semi-automatically
- Automatically
The correct level of automation depends on:
- Component geometry
- Lead structure
- Packaging
- Quantity per PCB
- Production volume
- Product mix
Not every THT component is suitable for automatic insertion.
Manual THT Insertion
Manual insertion can remain practical for:
- High-mix products
- Low component quantities
- Irregular components
- Frequent product changeovers
Workstations can be improved through:
- Material kitting
- Visual work instructions
- Component identification
- Guided insertion
- Ergonomic layout
The goal should be controlled and efficient manual work rather than automation for its own sake.
Automatic THT Insertion
Automatic insertion may be attractive when:
- Component design is suitable
- Packaging supports automatic feeding
- Production volume is high enough
- Product configuration is stable
However, automation economics should be calculated using the actual BOM.
A hybrid combination of automatic and manual insertion can be more practical for some industrial products.
Polarity and Orientation Control
Industrial PCBAs may contain polarized or orientation-sensitive components.
Controls can include:
- Clear PCB markings
- Material identification
- Work instructions
- Guided insertion
- Component verification
- Pre-solder inspection
Errors should ideally be detected before soldering.
Step 8: Wave Soldering
Wave soldering may be suitable when a PCB contains many compatible through-hole joints.
A typical process includes:
Fluxing → Preheating → Wave Soldering → Cooling
Important factors include:
- Flux application
- Preheating
- Solder temperature
- Conveyor speed
- Wave stability
- PCB orientation
- Component solderability
- Equipment maintenance
There is no universal soldering recipe suitable for every industrial PCB.
Step 9: Selective Soldering
Selective soldering may be preferable when:
- THT joints are localized
- Bottom-side SMT components are present
- Certain areas should avoid wave contact
- Product mix is high
- Manual soldering is becoming a bottleneck
A typical selective soldering process may include:
Fluxing → Preheating → Programmed Selective Soldering → Cooling → Inspection
The choice between wave and selective soldering should follow PCB design and production economics.
Wave vs Selective Soldering
PCB Pallets
Wave soldering pallets may be used for:
- Protecting selected areas
- Supporting PCBs
- Controlling solder exposure
However, pallets can add:
- Tooling cost
- Thermal mass
- Cleaning
- Maintenance
- Storage
Use them where the process requires them rather than automatically for every PCB.
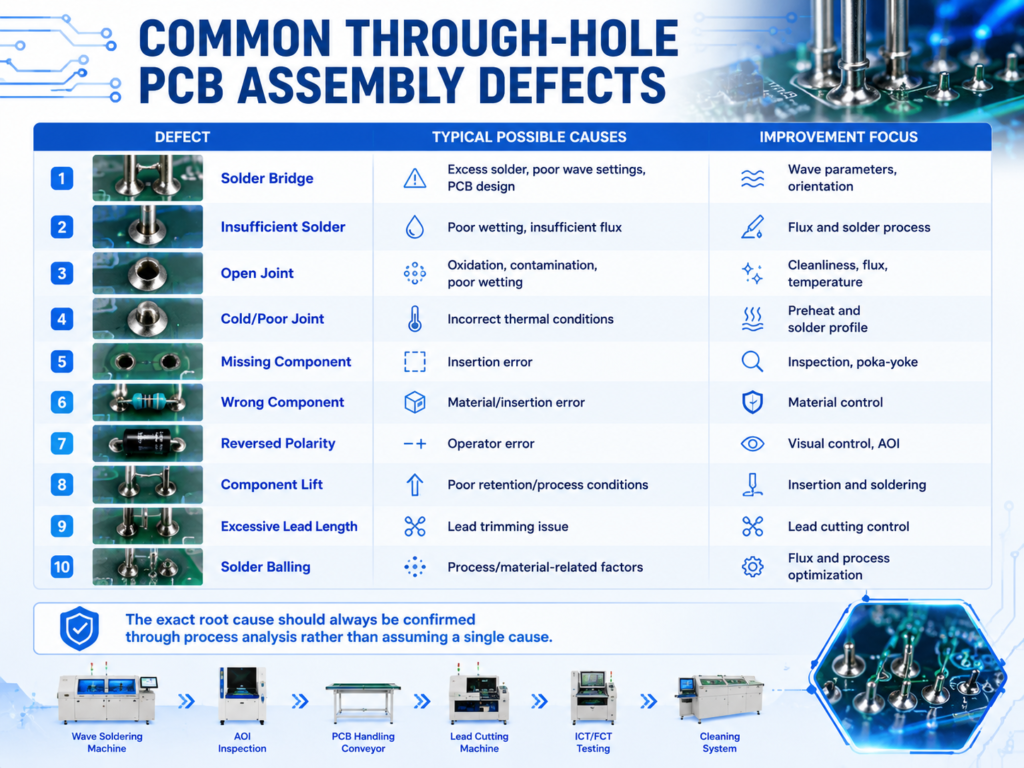
Common THT Soldering Defects
Potential defects include:
- Solder bridges
- Insufficient solder
- Poor wetting
- Incomplete hole fill
- Excessive solder
- Icicles
- Solder balls
Troubleshooting should consider the complete process:
PCB Design + Component Condition + Flux + Preheat + Solder + Conveyor + Equipment
Changing one parameter without identifying the root cause can create additional problems.
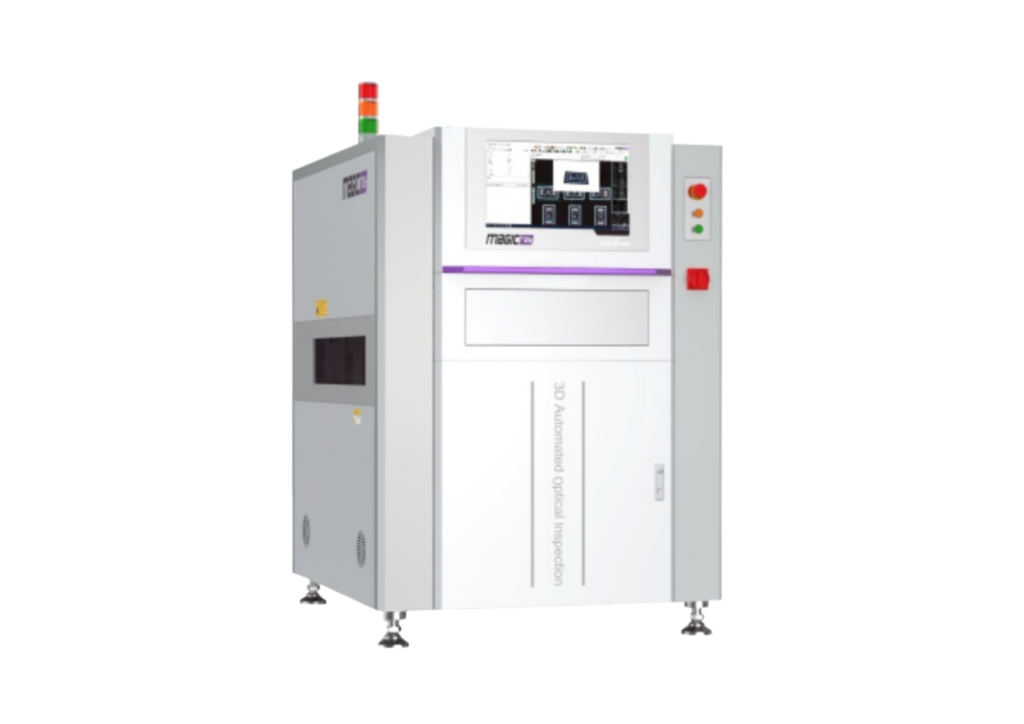
Step 10: Inspection
Inspection can include:
- Visual inspection
- AOI where applicable
- X-ray for selected hidden structures
- Electrical testing
Inspection should be designed around the actual defect risks and product requirements.
Step 11: Programming and Testing
Industrial automation PCBAs often require programming and functional verification.
Depending on the product, testing may include:
- ICT
- Flying probe
- Programming
- Functional testing
- Communication testing
- I/O testing
- Product-specific electrical tests
For example, a communication module may require different testing from a motor-control PCB.
The testing system should therefore be designed around product functionality.
Testing Can Become the Bottleneck
The complete line is approximately limited to: 40 boards/hour
Buying a faster placement machine would not solve this bottleneck.
Parallel Testing
Suppose functional testing requires:
- 90 seconds per board
- Required takt:
- 30 seconds
A simplified estimate is: 90 ÷ 30 = 3 parallel test positions
before allowing for loading, unloading, retest, and efficiency.
Testing should therefore be included in line-capacity planning from the beginning.
Traceability for Industrial Automation PCBAs
Depending on customer and product requirements, manufacturers may record:
- PCB serial number
- Product model
- Production time
- Machine
- Program
- Component information
- Material lot
- Solder paste information
- Inspection results
- Reflow process data
- Operator
- Test results
Barcode identification can connect production data across processes.
Not every industrial product requires the same traceability level.
Recipe Management
A mixed-production factory can have recipes for:
- Printer
- SPI
- Pick and place
- Reflow
- AOI
- Selective soldering
- Coating
- Testing
Product identification can help operators load the correct program.
Recipe management becomes increasingly important as product variety grows.
Conformal Coating for Industrial Automation PCBs
Some industrial automation PCBAs may require conformal coating depending on:
- Installation environment
- Humidity
- Condensation
- Dust
- Certain contaminants
- Enclosure
- Customer specification
A typical process may be:
Testing → Cleaning/Surface Preparation → Selective Coating → Inspection → Flash-Off → Curing → Final Inspection
However, not every industrial control PCB requires coating.
Selective Coating and Keep-Out Areas
Keep-out areas may include:
- Connectors
- Terminal contacts
- Test points
- Programming interfaces
- Switches
- Selected sensors
Automatic selective coating can reduce unnecessary application and masking.
However, masking may still be required for difficult geometry or sensitive areas.
Material Flow and WIP
A good PCBA line requires more than individual machines.
Plan material flow for:
- Bare PCBs
- SMT components
- THT components
- Feeders
- Trays
- Finished PCBAs
- NG boards
- Rework
Excessive WIP can hide production problems and consume floor space.
Insufficient buffer capacity can also cause upstream equipment to stop unnecessarily.
High-Mix Industrial Automation Line
A flexible configuration may use:
Loader → Automatic Printer → SPI → Flexible Pick and Place → Reflow → AOI → Manual/Semi-Automatic THT Insertion → Selective Soldering → Inspection → Flexible Testing
Priorities include:
- Changeover
- Feeder capacity
- Recipe management
- Flexible insertion
- Flexible testing
This can suit factories producing multiple industrial PCB models.
Medium-Volume Industrial Automation Line
A medium-volume configuration may use:
Automatic Loader → Automatic Printer → SPI → Pick and Place Machine(s) → Reflow → AOI → THT Preparation → Balanced Insertion Stations → Wave/Selective Soldering → Inspection → Testing
Automation should be added where it reduces the actual bottleneck.
Higher-Volume Production
For stable higher-volume products, manufacturers can evaluate:
Automatic Loading → Printing → SPI → Multiple Placement Machines → Reflow → AOI → Automatic/Semi-Automatic THT Insertion → Soldering → Inspection → Parallel Testing → Automatic Unloading
Barcode identification and traceability may also be integrated where required.
Line Balancing
The complete process should be evaluated as:
Printing → SPI → Placement → Reflow → AOI → THT → Soldering → Inspection → Testing
Useful production metrics include:
- Cycle time
- Takt time
- First-pass yield
- Downtime
- Changeover
- WIP
- Rework
- Equipment utilization
Optimizing only the SMT placement section does not necessarily improve finished output.
Factory Layout
A practical industrial PCBA factory can include:
- Incoming material area
- Material storage
- SMT line
- THT preparation
- THT insertion
- Soldering
- Inspection
- Testing
- Rework
- Coating where required
- Finished PCBA storage
The layout should support logical material flow and maintenance access.
Factory Utilities
Depending on the equipment, utilities may include:
- Electrical power
- Compressed air
- Exhaust
- HVAC/environmental control
- Nitrogen where required
- Network connections
- Wave/selective soldering and coating equipment can also have specific exhaust requirements.
- Utilities should be planned before machine installation.
New vs Pre-Owned SMT Equipment
Industrial automation manufacturers can consider both new and suitable pre-owned equipment.
Pre-owned international-brand machines can be attractive where:
- Production requirements are well understood
- Equipment condition is verified
- Spare parts are available
- Technical support is available
- Initial investment is important
New equipment may be attractive where:
- Current automation is required
- Very high utilization is planned
- New technology is needed
- Long-term platform standardization is important
- A hybrid new + pre-owned line can also be considered.
Total Cost of Ownership
Equipment price is only part of the investment.
A simplified model is:
PCBA Line TCO = Equipment + Installation + Feeders + Tooling + Utilities + Training + Spare Parts + Maintenance + Energy + Labor + Downtime + Process Losses
The lowest machine quotation does not necessarily create the lowest manufacturing cost.
Industrial Automation PCBA Solutions from Fuliu Electronics
Established in 2014, Fuliu Electronics is dedicated to providing customers with high-quality PCBA intelligent manufacturing solutions and services.
With extensive experience in the SMT industry, we specialize in dependable equipment, professional technical support, and complete SMT and PCBA production line solutions.
Our product portfolio includes SMT pick and place machines from Fuji, Panasonic, ASM, Yamaha, JUKI, and Hanwha, together with ERSA reflow ovens from Germany, MagicRay SPI/AOI inspection systems, automatic solder paste printers, supporting PCBA equipment, pre-owned SMT equipment, SMT spare parts, machine leasing, and maintenance services.
For industrial automation manufacturers, Fuliu Electronics can help evaluate the complete process:
SMT Assembly → Inspection → THT Assembly → Wave/Selective Soldering → Testing → Optional Conformal Coating
Key planning information includes:
- PCB and BOM
- Component range
- Placement quantity
- THT component packaging
- Target capacity
- Product mix
- Inspection strategy
- Soldering process
- Testing requirements
- Traceability
- Existing equipment
- Factory layout
- New/pre-owned strategy
- Automation level
- Investment budget
As part of our global growth strategy, Fuliu Electronics is actively expanding into international markets, with key focus areas including India, Vietnam, the Philippines, Indonesia, the Middle East, South Africa, and Europe.
Frequently Asked Questions
A line may include a solder paste printer, SPI, pick and place machines, reflow oven, AOI, THT preparation and insertion equipment, wave or selective soldering, inspection, and testing equipment.
Many designs do, although the exact combination varies. SMT can be used for dense control electronics, while THT may be used for selected connectors, relays, transformers, terminals, capacitors, and power components.
It depends on THT joint distribution, bottom-side component layout, production volume, and product mix. Wave can be efficient for many compatible joints, while selective soldering can suit localized THT areas.
Not universally. SPI can provide valuable information about the solder paste printing process, particularly for complex or fine-pitch assemblies.
No. X-ray is generally considered where hidden solder structures require inspection. The inspection plan should follow actual component and product requirements.
Yes, for suitable components and packaging. However, irregular components or high-mix products may still be better suited to manual or semi-automatic insertion.